About Sodium Hexa Meta Phospate
| Grade Standard |
Technical Grade |
| Physical Form |
Powder |
| Packaging Size |
25 kg |
| Usage |
Food additive, Industrial, Laboratory |
| Packaging Type |
HDPE Bag |
| Purity |
68% |
| Physical State |
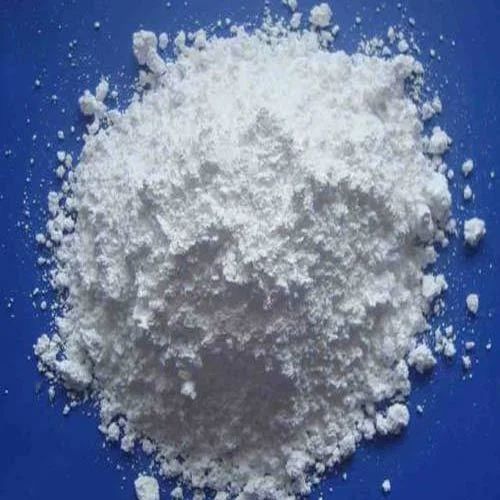
Powder |
| Molecular Formula |
(NaPO3)6 |
| CAS No |
10124-56-8 |
| Color |
White |
| Formula |
(NaPO3)6 |
| Packing Size |
25 Kg |
| Packing Type |
Bag |
| Molar Mass |
611.77 g/mol |
| ChemSpider |
23340 |
| EC Number |
233-343-1 |
| PubChem CID |
24968 |
| Density |
2.484 g/cm3 |
| Melting Point |
628 deg C (1,162 deg F, 901 K) |
| Boiling Point |
1,500 deg C (2,730 deg F, 1,770 K) |
We have been counted amongst the most trusted names in this domain, engaged in offering a standard quality range of these products.
Versatile ApplicationsSodium Hexametaphosphate stands out for its diverse uses. Whether it's improving water quality in treatment plants, ensuring smooth processing in the food industry, or enhancing performance in detergents and ceramics, SHMP delivers reliable results. Its properties as a dispersing agent and sequestrant make it indispensable across multiple industrial sectors.
High Purity and Quality StandardsProduced according to GB 1624-2005 and FCC standards, SHMP is available in both industrial and food-grade forms. Stringent limits on impurities-including low lead and iron content-ensure product safety and compliance for demanding applications, while its non-toxic and non-hazardous classification provides added assurance.
Ease of Use and Safe HandlingSHMP is stable, non-hazardous, and non-poisonous, suitable for both large-scale and small-scale operations. Being odorless and available in solid form, it is easy to handle, store, and transport. Its two-year shelf life ensures users have a dependable supply that maintains its quality under optimal storage conditions.
FAQ's of Sodium Hexa Meta Phospate:
Q: How should Sodium Hexametaphosphate be stored to maintain its stability?
A: Sodium Hexametaphosphate should be stored in a cool, dry place, away from sources of moisture and strong acids. Under recommended storage conditions, it remains stable and retains its effectiveness for up to two years.
Q: What are the primary uses and benefits of SHMP in industrial processes?
A: SHMP is widely used as a water softener, sequestrant, and dispersing agent. It helps prevent scale formation in water treatment, enhances dispersion in ceramics and detergents, and stabilizes processed foods, contributing to higher product quality and process efficiency.
Q: When is SHMP most beneficial in water treatment applications?
A: SHMP is most beneficial when used to control hardness and prevent precipitation of metal ions. Its ability to sequester calcium and magnesium ions improves water quality and protects equipment from scale build-up.
Q: What chemicals should SHMP not be mixed with for safety and performance reasons?
A: SHMP is compatible with most chemicals but should not be mixed with strong acids, as this can lead to decomposition and reduced effectiveness.
Q: Where can SHMP be safely applied in the food industry?
A: SHMP is approved for food-grade applications and can be used safely as a sequestrant and stabilizer in processed foods, provided purity standards are met. Its use is regulated and should comply with specific guidelines in each region.
Q: What is the process for dissolving SHMP in water for industrial use?
A: To dissolve SHMP, gradually add the powder or granules to water with stirring. It is easily soluble, forming a clear solution suitable for dispersing, softening, or stabilizing, depending on the intended industrial application.





 Send Inquiry
